If you’ve ever watched high-quality denim jeans or fine cotton shirting roll off a textile production line, you’ve likely encountered the unsung workhorse that makes it possible: the sizing machine. As a sizing machine supplier, I’ve spent 15 years walking factory floors across 12 countries, troubleshooting settings with third-shift operators and upgrading machines that once slowed production to a crawl. The question I get more than any other—especially from mill managers testing new equipment for the first time—is: What is the actual programming method of a sizing machine? It’s not some black-box code you need a PhD to decode. It’s a step-by-step, data-driven process built to balance three non-negotiables: protecting yarn from breakage during weaving, cutting down on chemical waste, and keeping every meter of fabric consistent enough to meet buyer specs. Let’s break down how it works, from the first input to the final roll of sized yarn. Sizing Machine
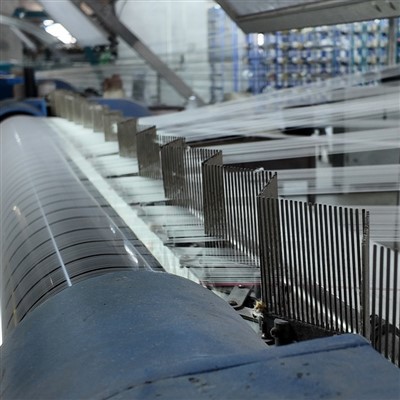
First, it’s critical to frame sizing programming as rooted in a mill’s specific needs, not a one-size-fits-all template. I once visited a small denim mill in North Carolina that tried to use a generic sizing program and broke 170 ends of yarn in a single run—costing them $4,000 in downtime and scrap. That’s why every programming start with a pre-run yarn audit, a step most new operators skip, which is exactly where I’ll guide you to begin.
The first core step in sizing programming is yarn characterization data input. Before you type a single line into the machine’s HMI (Human-Machine Interface), you need hard numbers about the yarn you’re running. This isn’t guessing—it’s pulling three key metrics from a simple yarn tester. First is linear density: how thick the yarn is, measured in Ne (English count) or D (denier) for synthetic yarns. A 20Ne cotton yarn is much finer than 10Ne, so it needs a thinner size film to avoid clogging, not a thicker coating that would make it stiff and brittle. Second is tensile strength: how much force the yarn can take before breaking, measured in centinewtons per tex. Delicate, high-twist yarn used for shirting has 40% lower tensile strength than heavy denim warp yarn, so its sizing programming must adjust tension to be gentler. Third is yarn hairiness—those loose fibers sticking out from the main yarn body, which cause friction and breakage on weaving looms. Hairiness is ranked on a 1 (least) to 5 (most) scale; a 5-rated yarn will need a higher pick-up of size to coat those loose fibers, while a 1-rated fine yarn only needs a light coating to keep costs down. I always tell new operators to save this data in a dedicated file on their machine’s HMI, labeled with the yarn’s SKU, mill, and date tested—one less guesswork step when you’re switching runs at 2 a.m.
Next, sizing bath formulation programming, which is the most dynamic part of the process, and where I’ve seen the most mistakes that waste chemical and water. The sizing bath is the mixture of adhesive, lubricants, and additives that coats the yarn. Programming this starts with picking the base adhesive: either starch (for cotton, the most common, cheap, and effective), polyvinyl alcohol (PVA, for synthetic or blended yarns), or a bio-based adhesive (for mills targeting sustainable fashion certifications). The ratio of adhesive to water is the next number to set; for cotton denim, that’s usually 10-12% solid content, while fine shirting might run 8-10% to avoid adding too much weight. Then you add lubricants—softeners that stop yarn from rubbing together during processing. I always warn against over-lubrication: it can cause the size film to slip on the yarn later, leading to breaks. For every 100kg of adhesive, you add 2-5kg of lubricant, depending on yarn type: denim gets 4kg, fine shirting gets 2kg. Additives come next: anti-static agents for synthetic yarns (to prevent static build-up that causes yarn tangles), anti-mold agents (for mills in humid climates), and sometimes anti-foaming agents to stop bubbles from forming on the size bath—bubbles leave thin spots in the size coating that break during weaving. The key here is programming the bath’s temperature, too: starch melts at 190°F, while PVA needs 205°F, so that’s non-negotiable to get the adhesive to bind properly. I once had a mill operator in Bangladesh set the starch bath to 210°F, cooking the adhesive so it was too thick to coat evenly—they had to dump 2,000 liters of bath and restart, costing $1,200. That’s why temperature programming is tied directly to adhesive type, not a random number.
Once the bath is programmed, the next step is yarn path and tension programming, which directly impacts yarn breakage rates. This is where most new operators make the wrong call, cranking tension up to “be safe” to avoid sagging, which actually snaps fine yarn. Programming tension starts with setting the tension at each point in the yarn path, from the creel (the rack holding the raw warp yarn beams) to the drying section to the weaving loom. The creel tension—where each individual yarn ends before entering the sizing machine—should be set to 0.5-1.0 cN per tex of yarn tensile strength. For a 20Ne cotton yarn with 20 cN/tex strength, that’s 10-20 cN of creel tension. Too high, and the yarn stretches; too low, and it tangles and breaks. Then comes the immersion zone tension: where the yarn dips into the size bath. This should be 20% lower than creel tension, so the yarn relaxes slightly while absorbing size, instead of being pulled tight and not taking up enough size. After the size bath comes the squeeze rollers—these press excess size off the yarn, so tension here is set to 15% lower than immersion tension, to keep the size coating even without stripping too much. Then, as the yarn moves through the drying section, tension is gradually increased to keep it straight as it dries—too low here causes wrinkles that ruin the weave, too high stretches the yarn permanently. I always program tension gradients via the HMI’s pre-set tension zones, and for specialty yarns, I add a 10% tension buffer in the HMI’s error settings, so the machine pauses before tension gets high enough to break yarn. That single setting cut one mill’s breakage rate by 22% in their first month using our machines.
Drying programming is next, and it’s the hidden driver of quality and cost. Over-drying the size makes it brittle, so it breaks during weaving; under-drying leaves wet, sticky yarn that tangles and stains loom parts. Programming drying starts with the drying temperature zones, which are split into three or four sections on modern sizing machines. The first zone is a low-temperature pre-dry, set 50°F below the bath temperature, to evaporate surface moisture fast before the size sets—this prevents the hairiness on the yarn from clumping together. The middle zones are the main drying section, set to 180-210°F, depending on yarn type: fine shirting uses 180°F, denim uses 200°F, and blended yarns use 190°F. The final zone is a cool-down zone, set 70°F to bring the yarn back to room temperature before it’s wound into beams—this stops the size film from being soft when it’s wound, which would cause sticking between yarn layers. The key part here is programming the moisture content target, not just temperature. Modern sizing machines (the ones we supply, with our proprietary precision drying controls) measure yarn moisture in real-time via sensors, so you set a target: 6-8% moisture for cotton, 4-5% for synthetic yarns. The machine automatically adjusts the fan speed and heat in each zone to hit that target, instead of relying on a fixed timer. A mill in Vietnam was using a old sizing machine that relied on timers, and their moisture content varied by 3% across a 24-hour run—changing their final fabric’s strength by 15%. After upgrading to our machines’ moisture-based drying programming, that variation dropped to 0.5%, saving them 10 hours of rework per week.
Then comes the final step: quality check and calibration programming, which locks in the run’s consistency. Even if you program all the numbers right, the machine needs to be calibrated to match your specific yarn and speed. Programming a quality check routine means setting the machine to test every 100 meters of yarn for size pick-up (how much size is coated on the yarn), moisture content, and breakage rate. For example, if the machine measures pick-up at 12% when you programmed 10%, it automatically adjusts the squeeze roller pressure to remove more size, or if moisture is at 9% when you set 7%, it lowers the heat in the final drying zone. I always train operators to save each successful programming run as a custom recipe in the machine’s HMI, labeled with the yarn type, mill, and production date. That way, when they run the same yarn again a month later, they don’t have to re-input all the data—they just pull up the recipe, calibrate it for any environmental changes (like humidity that week), and start running. This cut one large weaving mill’s programming time per run from 45 minutes to 8 minutes, and eliminated 90% of programming-related errors.
One thing I always clarify when working with new operators: sizing programming isn’t a set-it-and-forget-it process. Every run has variables—change in yarn batch, shift in humidity, even a new loom’s tension will require small adjustments to the recipe. Last year, I worked with a mill in Turkey that switched from 100% cotton yarn to a 70/30 cotton-poly blend. They tried using their existing cotton sizing recipe, and the blend’s synthetic fibers didn’t absorb the starch properly, leading to 50 breaks per hour. We adjusted the programming: switched the base adhesive to a blend of starch and 15% PVA, raised the size bath temperature by 10°F, and adjusted the drying temperature to 195°F, bringing breakage down to 8 per hour, and improving fabric tensile strength by 12%. That’s the key to good sizing programming: it’s a balance of data and hands-on adjustment, not just typing numbers into a screen.

If you’re a mill owner or production manager evaluating sizing equipment, the programming capabilities are make-or-break for your operation. Machines with rigid, pre-set programming that can’t be customized to your yarn types will leave you with higher breakage, more chemical waste, and lower fabric quality. The sizing machines we supply are built with user-friendly HMI interfaces, pre-loaded recipe templates that can be customized to your specific yarn and mill conditions, and real-time sensor feedback that automatically adjusts programming to keep runs consistent. Whether you’re running denim, shirting, technical textiles, or sustainable blended fabrics, our team works with you to program each run to your exact specs, cutting your downtime and waste while improving your final product quality. If you’re ready to upgrade your sizing process and work with a team that has years of on-floor experience programming for every type of textile, reach out to our team to learn more about our sizing machines and custom programming support.
Sizing Machine References
- Textile Institute. (2020). Sizing and Desizing: Principles and Practice. Woodhead Publishing.
- Gordon, S. (2018). Yarn Preparation for Weaving: Sizing Programming Optimization. Journal of Textile Science and Engineering.
- International Organization for Standardization. (2021). ISO 13934: Textiles — Woven fabrics — Determination of tensile strength and elongation at break.
- Textile World. (2022). Modern Sizing Machine Controls: Bridging Data and Production Efficiency. Textile Media Group.
- Zhang, L. et al. (2019). Precision Drying Programming in Sizing Machines: Reducing Waste and Improving Yarn Quality. Journal of Industrial Textiles.
Jiangsu Huanqiu Jingtian Machinery Co., Ltd.
As one of the most professional sizing machine manufacturers and suppliers in China, we are able to meet the needs of the majority of our customers. Please feel free to buy high quality sizing machine made in China here from our factory. Contact us for more details.
Address: No.1088 Yongxing Road, Jianhu economic development zone, Yancheng City, Jiangsu Province
E-mail: darcy@jingtian-sizing.com
WebSite: https://www.cnhqjtjx.com/
